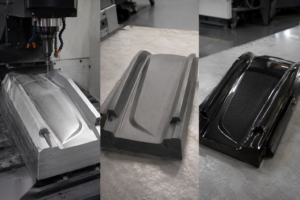
Carbon fiber is a fiber material that can greatly improve the performance of automobiles. It is generally used in various parts of the car body, such as bumpers, rearview mirrors, spoilers, and so on. It can not only increase the hardness of the car body, but also greatly reduce the weight of the car body, and reduce the maintenance cost of the car body. It can be said to be a material with huge returns for a small investment.
This article will give everyone a detailed breakdown of the material “carbon fiber”.

What is Carbon Fiber?
Carbon Fiber (CF for short) is a high-performance fiber material made from organic precursor fibers such as polyacrylonitrile (PAN) or pitch, through a carbonization process at high temperature in an inert environment. Its carbon content is usually above 90%, and can even reach as high as 99%. The diameter of a single carbon fiber filament is only about 5-10 microns, almost one tenth of a human hair.

Inside, the carbon atoms are highly parallel arranged in crystal form along the long axis of the fiber, forming a hexagonal ring-shaped graphitized structure. It is this stable structure that gives carbon fiber components extremely high strength. Carbon fiber, just as its name implies, not only has the functional characteristics of carbon materials, but also has the soft characteristics of textile fibers, making it extremely malleable.
The tensile strength of carbon fiber is 5-10 times that of ordinary steel, but its density is only about 1/4 of steel (about 1.5-2.0 g/cm³). Compared with steel of the same weight, the structural strength of carbon fiber is much higher.
Extremely high strength and extremely light weight—the combination of these two makes carbon fiber material almost perfect. In addition, carbon fiber also has the advantages of high elastic modulus, excellent corrosion resistance, high temperature tolerance (above 2000°C in non-oxidizing environments), and extremely low thermal expansion coefficient. It is not easy to deform even when temperature changes rapidly from high to low, which is the icing on the cake for this material.
In the market, fiber bundles formed by collecting thousands of filaments are commonly used.

These fiber bundles can be used alone, or can be woven into carbon fiber cloth, or can be composited with matrix materials such as resin, metal, and ceramics to make carbon fiber reinforced polymer (CFRP). Among them, carbon fiber reinforced polymer (CFRP) is currently the most widely used form, accounting for more than 90%.
This kind of composite material not only fully retains the core advantages of carbon fiber such as high strength, high modulus, and low density, but also has the forming convenience and corrosion resistance of the matrix materials. It is an ideal choice to replace traditional metal materials. Because of these outstanding advantages, carbon fiber is called “the king of new materials” and “black gold” by the industry, and is widely used in aerospace, automobile manufacturing, wind power energy, sports and leisure, and high-end industrial fields. It has become an irreplaceable choice.

Properties of Carbon Fiber
Performance Feature | Content |
|---|---|
Low Density | Bulk density 1.8 g/cm³. The density of carbon fiber composite is basically equivalent to magnesium and titanium, less than 1/4 of steel, and 1/2 of aluminum alloy. Using carbon fiber composite as structural material can reduce structural weight by 30%–40%. |
High Tensile Strength | Tensile strength above 3500 MPa. |
High Modulus | Elastic modulus above 230 GPa. |
High Specific Strength | Specific strength 1900 MPa/Kg, 16 times greater than steel, 12 times greater than aluminum alloy. |
Ultra-High Temperature Resistance | Under non-oxidizing atmosphere, can be used at 2000°C. |
Low Temperature Resistance | At -180°C low temperature, steel becomes more brittle than glass, while carbon fiber still maintains elasticity. |
Acid, Oil, and Corrosion Resistance | Carbon fiber has high pure carbon content, and carbon is one of the most stable chemical elements, causing it to withstand erosion from concentrated hydrochloric acid, phosphoric acid, and other media. Its corrosion resistance exceeds gold and platinum, while also having good oil resistance. |
Low Coefficient of Thermal Expansion | Most carbon fibers have negative coefficient of thermal expansion at room temperature, zero at 200–400°C, and only 1.5×10⁻⁶/°C below 1000°C, not easily deformed due to high working temperature. |
Strong Fatigue Resistance | Carbon fiber structure is stable. According to Polymer Network statistics, after millions of cycles of stress fatigue testing, its composite material still retains 60% of strength, while steel is 40%, aluminum 30%, and fiberglass only 20%–25%. |
Manufacturing Process of Carbon Fiber
In the production practice of JC Autocarbon, we deeply realize: the birth of a high-quality carbon fiber is by no means simple “high-temperature firing,” but a systematic engineering involving polymer chemistry, precision spinning, and extreme heat treatment. Currently, over 90% of industrial carbon fibers originate from the Polyacrylonitrile (PAN) route. The length of its preparation chain and the narrowness of its process window constitute the core of this material’s high technical barrier.
Monomer Polymerization
Acrylonitrile → PAN
Spinning & Forming
Wet / Dry-jet Wet
Pre-oxidation
200–300°C · Air
Carbonization
1000–1500°C · Inert Gas
Graphitization
2000–3000°C · Optional
Surface Treatment
Sizing · Winding
1. Polymerization and Spinning: The Starting Point of Establishing Microscopic Order
Everything starts from the petroleum cracking product — propylene. After obtaining high-purity acrylonitrile monomer (purity needs to reach above 99.9%) through ammoxidation reaction, free radical polymerization is carried out under the action of initiator to generate polyacrylonitrile resin with controllable molecular weight.
Subsequently, the resin is dissolved in solvents such as dimethyl sulfoxide (DMSO) to form spinning solution, which is extruded and formed through wet spinning or dry-jet wet spinning process. Dry-jet wet spinning has become the mainstream technical route for high-performance carbon fiber precursor because of its higher spinning speed (can reach above 300 m/min) and more rounded and dense fiber cross-section.
The formed precursor needs to go through washing, stretching, and drying, finally obtaining white PAN precursor with diameter about 10–15 microns. This white PAN precursor is the source of carbon fiber’s high strength.
2. Pre-oxidation: The Key Transformation from Organic to Inorganic
Pre-oxidation is the most time-consuming and energy-consuming link in the entire production line, usually occupying 75%–90% of total processing time. The precursor is slowly heated to 200–300°C at a rate of 1–5°C/min under controlled tension. Oxygen in the air promotes cyclization and cross-linking of the cyano groups in the PAN molecular chain, forming heat-resistant ladder structure.
This process releases large amounts of volatile gases such as NH₃ and HCN, and the fiber color also changes from white to yellow, brown, and finally deep black.
If heating is too fast or tension is uneven, the fiber is very easy to fuse and be scrapped. The uniformity of pre-oxidation directly determines the skin-core structure ratio and mechanical consistency of the final carbon fiber, which is exactly the link that JC Autocarbon particularly values in quality control.
3. Carbonization: The Leap of Carbon Content
The pre-oxidized fiber enters a carbonization furnace filled with nitrogen protection, experiencing two stages of pyrolysis: low-temperature carbonization (400–800°C) to expel residual non-carbon elements such as hydrogen, oxygen, and nitrogen; high-temperature carbonization (1000–1500°C) further regularizes the carbon plane structure, causing carbon content to leap to above 95%.
After this step, fiber density increases from about 1.2 g/cm³ to 1.7–1.9 g/cm³, and strength obtains a qualitative leap.
4. Graphitization and Post-Treatment: The Ultimate Tuning of Performance
If high-modulus carbon fiber (elastic modulus >350 GPa) needs to be prepared, then graphitization treatment (2000–3000°C) must be carried out in argon atmosphere. High temperature promotes graphite crystallites to highly orient and arrange along the fiber axial direction, and modulus can soar to 500–600 GPa, but strength will slightly decrease.
Subsequently, the fiber undergoes electrolytic oxidation for surface roughening and functional group modification to improve interfacial bonding force with the resin matrix; finally, epoxy resin or polyurethane-type sizing agent is coated, and it is wound into a roll. At this point, the production of high-quality carbon fiber tow is completed.

Practical Applications of Carbon Fiber
Carbon fiber is rarely used alone. The more common application is the composite material system (CFRP) formed after fusing it with resin, metal, ceramic, and other materials. The strength and modulus of CFRP are both unparalleled, so its applications in various industries are extremely wide.
✈️
Aerospace
Carbon fiber is the core weight-reducing material for commercial aircraft fuselage, wing primary load-bearing structures, and engine components. The carbon fiber usage of Boeing 787 and Airbus A350 respectively reaches 50% and 53% of the total aircraft weight. Each aircraft can reduce weight by several tons, and fuel efficiency improves by more than 20%.
🚗
Automotive and Racing
From F1 monocoque to mass-produced supercar body structural parts, and then to electric vehicle battery pack enclosures, all use carbon fiber. Carbon fiber battery pack can reduce weight by more than 40% compared with aluminum alloy, and 10% vehicle weight reduction can bring 6%–8% range improvement.
🌬️
Wind Energy
Carbon fiber is the core material for the spar cap of hundred-meter-level wind turbine blades. Carbon fiber can make blades longer, lighter, and stiffer, significantly improving swept area and power generation efficiency, and has become the standard configuration for offshore large-megawatt units.
⚽
Sports and Leisure
Carbon fiber material can reduce golf club weight by nearly 50%, and bicycle frame weight by nearly 40%. Tennis rackets, fishing rods, skis, and other products using carbon fiber can also obtain lighter hand feel and more precise body feeling.
🏥
Medical and Health
Carbon fiber has excellent X-ray penetrability (almost does not absorb rays), so it is widely used for CT bed plates, surgical instruments, and orthopedic implant brackets. PEEK-based thermoplastic carbon fiber also has good biocompatibility.
⚙️
Hydrogen Energy and Industry
Carbon fiber is the core winding layer material for Type IV hydrogen storage cylinders. It can ensure safe hydrogen storage and transportation under 70 MPa high pressure. It is also applied to robotic arms, drones, precision instrument brackets, and other scenarios with extreme requirements for stiffness and weight reduction.


Comparison of Carbon Fiber with Other Materials
At the material selection stage, the question customers ask most often is: “How much better is carbon fiber than the steel/aluminum/fiberglass I am currently using?” The answer cannot be generalized, but data does not lie. The table below systematically compares Carbon Fiber Reinforced Polymer (CFRP) with traditional metal materials and fiberglass from the perspective of key engineering indicators.


Comparison Dimension | Carbon Fiber (CFRP) | High-Strength Steel | Aluminum Alloy (6061-T6) | Titanium Alloy (TC4) | Glass Fiber (GFRP) |
|---|---|---|---|---|---|
Density (g/cm³) | 1.5–1.65 | 7.85 | 2.70 | 4.5 | 2.0 |
Tensile Strength (MPa) | 1500–2800+ | 980–1080 | 310 | 960 | 1500 |
Specific Strength (×10⁴) | 10–18+ | 1.3 | 1.15 | 2.1 | 4.8 |
Elastic Modulus (GPa) | 230–600 | 210 | 69 | 114 | 42 |
Specific Modulus (×10⁶) | 8.6–24 | 2.6 | 2.6 | 2.5 | 2.1 |
Thermal Expansion Coefficient (10⁻⁶/°C) | −1.2 ~ 1.0 (Designable) | 12 | 23.6 | 8.6 | 5–7 |
Fatigue Resistance | Excellent | General | General | Good | Good |
Corrosion Resistance | Excellent (No Coating Needed) | Needs Galvanizing / E-coating | Needs Anodizing | Excellent | Excellent |
Material Unit Price | High | Low | Medium | High | Low |
Typical Weight Reduction Potential vs Steel | 50–70% | — | 30–50% | 40–50% | 25–40% |
Recyclability | Recyclable but High Energy Consumption | Fully Recyclable | Fully Recyclable | Fully Recyclable | Recyclable |
How to Read This Table?
From the table it can be seen that carbon fiber crushes other metal materials in strength and modulus. For example, if a car’s structural parts are completely replaced from steel to carbon fiber, then the weight of this car can almost be reduced by half, and the body strength does not decrease but instead increases.
However, carbon fiber is also not suitable for all situations. Its anisotropy means that mechanical properties highly depend on the fiber layup direction; transverse and interlaminar shear strength are far lower than axial tensile strength, which needs to be compensated through precise layup design.
In addition, the brittle failure mode of carbon fiber (fracture without plastic deformation warning) and the lightning strike protection and galvanic corrosion problems brought by conductivity also require engineers to take them into consideration at the design stage.
In the customization process of JC Autocarbon, we always advise customers to adopt a “scenario matching” mindset: for load-bearing parts that are extremely cost-sensitive and have simple shapes, steel, aluminum, or composite parts combining metal with carbon fiber are more practical choices; for high-end structures pursuing extreme weight reduction, high fatigue life, or complex curved surfaces, the advantage of carbon fiber is irreplaceable.
FAQ
Not sure which process fits your project?
Send us your part drawings or a sample
Our engineering team will review it and recommend the most cost-effective route.
Want to keep reading? Browse the full Resource Center for more articles, installation guides, and pricing insights from the factory.
Author: He Dong
He Dong – Automotive & Motorcycle Engineering Specialist, has spent 20+ years doing what he loves most — making cars and bikes faster, sharper, and better looking.